
What Is Let Down Ratio (LDR) in Plastic Injection Molding?
Master-batch is added to resin during molding to give plastic products their color. Let-Down Ratio (LDR) is the ratio of master-batch to base resin. It determines the color intensity, the uniformity and the final aspect of the molded product.
Key Factors That Decide Colored Plastics Let Down Ratio
The required LDR is a function of several variables:
Required Color Shade Depth
Product volume and geometry
Natural color of base resin
master batch, liquid or solid
All of these factors play a role in how much pigment is required to achieve the desired visual output.
Typical Let Down Ratios For Small And Large Plastic Products
LDR may differ depending on product size and application.
Example:
A typical 400 ml shampoo bottle cap consumes 0.5% – 2% LDR.
30 liter bucket may need 2% – 4% LDR.
Generally, larger parts or darker shades require higher master-batch concentrations.
Deciphering “Let Down Ratio” in Post-Consumer Resin (PCR)
When using recycled plastic grains or Post-Consumer Resin (PCR), LDR behaves differently from virgin resin. Moreover, PCR presents additional challenges in terms of color uniformity and esthetic appeal.
Problems with the Physical Appearance and Coloring of PCR Materials
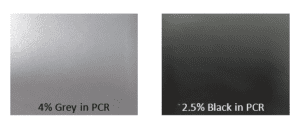
The polypropylene (PP) PCR available on the market usually has a natural, non-uniform gray appearance when molded without master-batch. Market surveys have shown that this raw gray look is not attractive to consumers especially in FMCG packaging applications.
PCR product, impact of master-batch dye choice
Adding bright colors such as white, yellow or blue at standard LDR levels (0.5% – 2%) often results in a pale gray, pale yellow or pale bluish gray color.
These results are not very pretty. Hence darker colors such as black, shiny gray or dark blue are often chosen to mask the inherent gray tone of PCR.
Why PCR needs higher Let Down Ratio than Virgin Resin
Even with darker master-batch colors standard LDR levels may not provide sufficient depth or uniformity in PCR products.
Consequently, LDR is frequently raised from 0.5%–2% to 2%–5%, depending on part geometry and desired color depth. This compensates for the variation of recycled resin and gray tone.
The effect of an increase in let down ratio on processing conditions
In most cases, the increase of LDR does not need significant modification of the processing conditions.
However, it is sometimes necessary to adjust the hot runner manifold tip temperature so that the flow and color dispersion are correct, especially in thermally operated hot tip systems.
High LDR in PCR and Resulting Flow Marks and Surface Defects
More quality complications can occur when LDR > 5%.
As the molten PCR-master-batch mixture flows in the hot tip toward the cavity, flow marks can appear around the gate area. This is especially the case of shiny or pearlized master-batches that accentuate flow lines even more.
Scuff Marks, Pigmentation & Gate Blush Sensitivity Demystified
Higher master-batch content leads to higher pigmentation and makes the surface more sensitive to external forces.
The common defects are:
Scuffing or rubbing marks from part ejection
Gate blush (glossy patch near the gate)
Surface defects related to pigment concentration
These problems are difficult to eliminate completely and tend to persist.
Higher Let Down Ratio in Recycled Plastics – Cost Implications
Increasing the LDR will have a huge effect on cost per piece. Master-batch materials increase raw material costs, and higher concentrations directly increase overall production cost.
Hence, the use of PCR calls for careful balancing of color performance and economic feasibility.
Balancing Aesthetics, Cost and Sustainability in PCR Packaging
Recycled resin in FMCG packaging can be a positive step toward environmental responsibility despite minor esthetic flaws.
EIPL is a specialist in sustainable product design and development. The company provides complete solutions in design, redesign, innovation and industrial tool qualification.
14+ years of global experience across 44+ countries. We help implement PCR, optimize cost, validate dimensional and functional performance, and ensure seamless execution of projects.
For more details www.efficientinnovations.in
FAQs
- What is let down ratio in plastic injection molding?
Let Down Ratio (LDR) The Let Down Ratio is the quantity of master-batch mixed with the base resin to achieve the desired color in a molded plastic part. It controls the color uniformity, visual appearance and intensity of shade of the final product.
- The let down ratio is higher in the post consumer resin.
Post-consumer resin (PCR) is naturally gray and the base color is not uniform. Often this masking effect and the resulting acceptable color depth and uniformity will require a greater concentration of master-batch than virgin resin.
- What are the normal let down ratios for PCR products?
For PCR products LDR is usually between 2% and 5% based on part geometry and desired shade. This is typically higher than the 0.5%–2% level typically used for virgin resin applications.
- What is the effect of LDR on color consistency in recycled plastics?
Higher LDR enhances color masking and depth in PCR, but uniformity may still be a problem due to differences in the base resin. Too little LDR can cause light or uneven shades.
- Does increasing let down ratio affect processing conditions?
There is no change in processing conditions. It may be necessary, e.g., to raise the temperature of the hot runner tip to get good dispersion of the pigment and stable flow.
- What are the surface defects of PCR with high let down ratio?
Visible flow marks around the gate, gate blush, shiny patches and scuff marks can be produced by high LDR. Additional pigmentation may also make the surface more susceptible to rubbing during ejection.
- How does let down ratio affect cost per molded part
The higher the LDR, the higher the material cost because master-batch is added to the raw material cost. The higher the percentage, the higher the cost per piece, which can be significant in high volume FMCG packaging.
- Recycled FMCG packaging: are visual defects acceptable?
Sustainable packaging initiatives may allow for minor variations in appearance. Environmental PCR products are often sold with some degree of tolerance for minor visual imperfections, provided the quality standards are met.